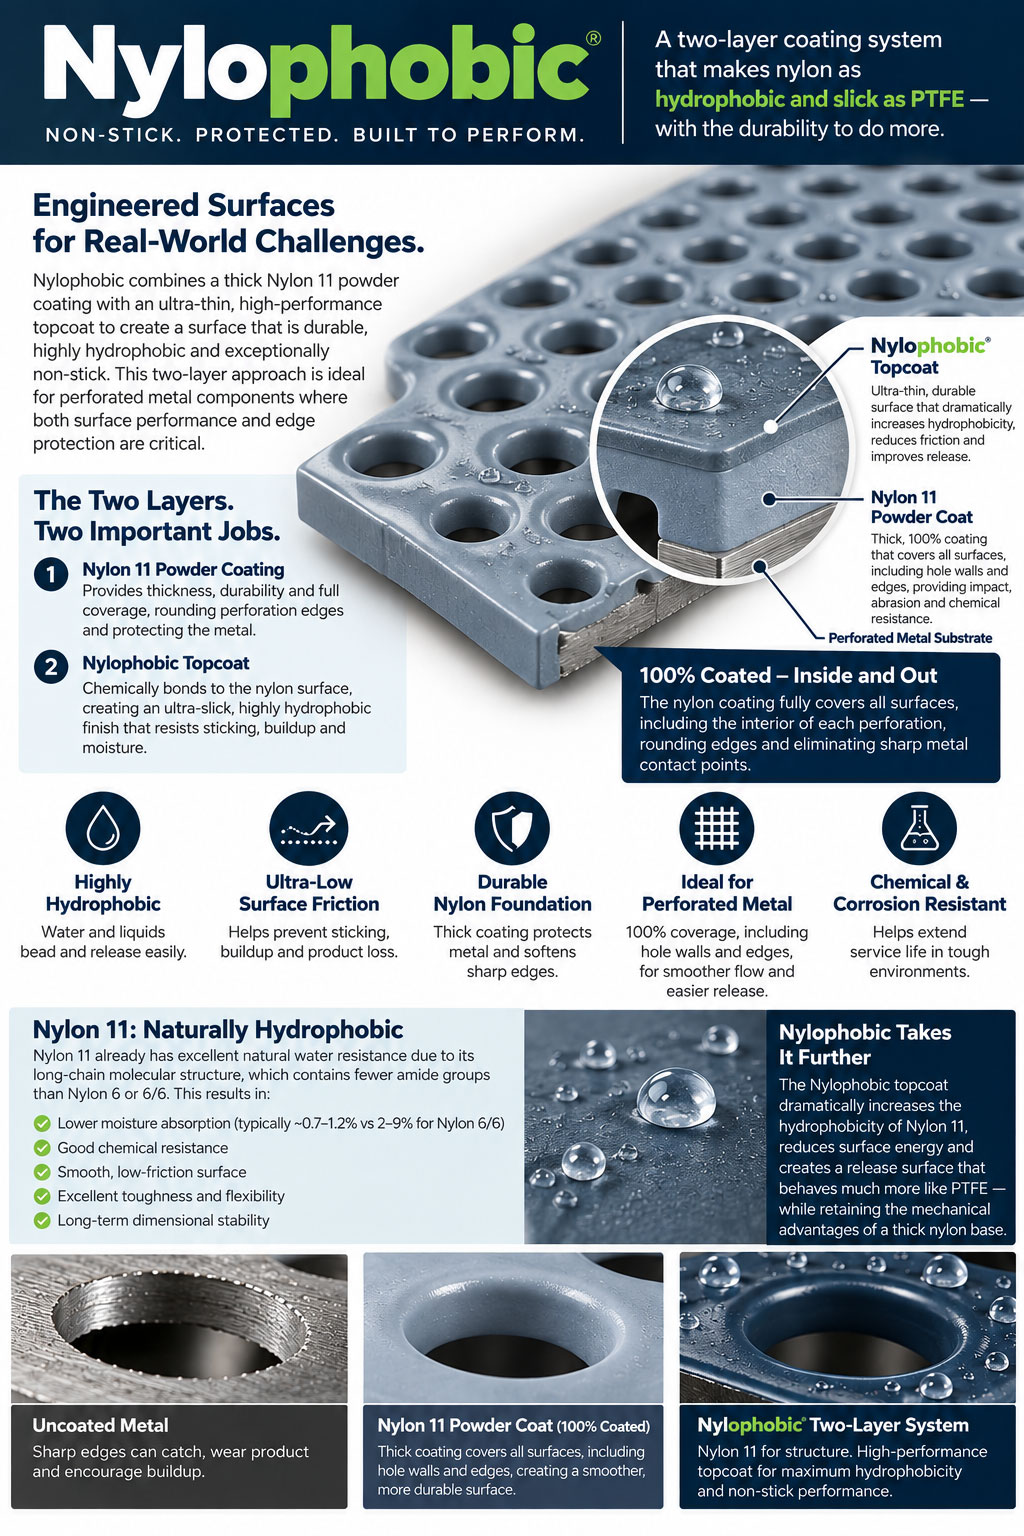
Nylophobic®: Making Nylon as Slick as PTFE, With the Durability to Do MorePerforated metal is everywhere in industrial processing: screens, trays, guards, conveyor components, drying racks. It is also one of the hardest parts to protect. Every hole has two sharp edges, a wall that is hard to reach, and a surface that loves to hold onto water, lint, and product.

Most coatings force a trade-off. Thick films protect the metal but can be tacky or absorb moisture. Slick, low-energy finishes like PTFE release well but are thin and give up durability. Nylophobic® is our answer to that trade-off: a two-layer system that makes nylon as hydrophobic and slick as PTFE, while keeping the toughness of a thick nylon base.

Two layers, two important jobs

Nylophobic pairs a thick Nylon 11 powder coating with an ultra-thin, high-performance topcoat. Each layer does something the other can’t.

Layer 1: Nylon 11 powder coating. This is the structure. It provides thickness, durability, and full coverage. It rounds perforation edges, protects the metal, and gives the part its impact, abrasion, and chemical resistance.

Layer 2: Nylophobic topcoat. This is the surface. It chemically bonds to the nylon and creates an ultra-slick, highly hydrophobic finish that resists sticking, buildup, and moisture. It dramatically increases hydrophobicity, reduces friction, and improves release.

Nylon 11 for structure. A high-performance topcoat for maximum hydrophobicity and non-stick performance.
Nylophobic®: Making Nylon as Slick as PTFE, With the Durability to Do More

Why start with Nylon 11?

Nylon 11 is already naturally water-resistant. Its long-chain molecular structure contains fewer amide groups than Nylon 6 or 6/6, and that difference shows up in performance:

  • Lower moisture absorption (typically about 0.7 to 1.2%, compared with 2 to 9% for Nylon 6/6)
  • Good chemical resistance
  • Smooth, low-friction surface
  • Excellent toughness and flexibility
  • Long-term dimensional stability

That makes Nylon 11 a strong foundation on its own. Nylophobic takes it further. The topcoat reduces surface energy and creates a release surface that behaves much more like PTFE, while keeping every mechanical advantage of the thick nylon underneath.

100% coated, inside and out

On perforated metal, coverage is where coatings usually fall short. Spray a sheet and the flats look great, but the hole walls and edges end up thin or bare. Those are exactly the spots where corrosion starts and where product catches.

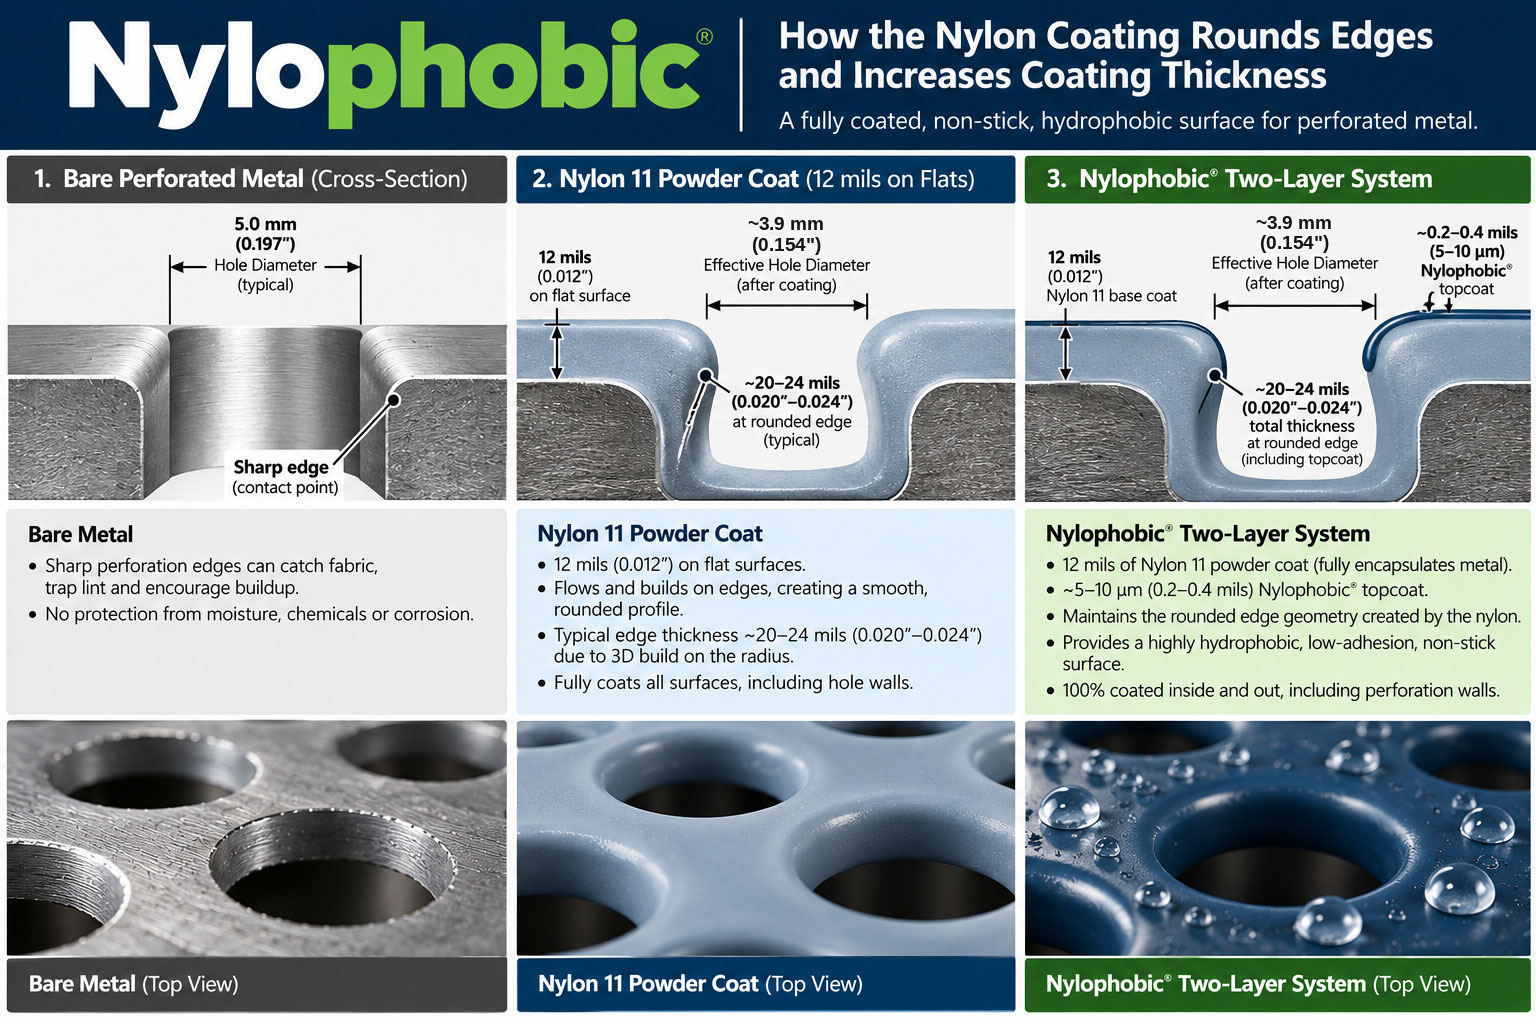
Nylon 11 powder coating fully covers every surface, including the interior of each perforation. As it cures, the nylon flows and builds on the edges, creating a smooth, rounded profile and eliminating sharp metal contact points.

Here is what that looks like in numbers on a typical part:

  • Flat surfaces: about 12 mils (0.012″) of Nylon 11
  • Rounded edges: about 20 to 24 mils (0.020″ to 0.024″), because the coating builds three-dimensionally on the radius
  • Nylophobic topcoat: about 5 to 10 µm (0.2 to 0.4 mils), thin enough to preserve the rounded edge geometry the nylon creates
  • Effective hole diameter: a typical 5.0 mm (0.197″) perforation finishes at about 3.9 mm (0.154″) after coating

That last point matters in design. If open area or flow rate is critical, plan the perforation size with the coating build in mind.

Uncoated vs. nylon vs. Nylophobic

Uncoated metal. Sharp perforation edges can catch fabric, wear product, trap lint, and encourage buildup. There is no protection from moisture, chemicals, or corrosion.

Nylon 11 powder coat. A thick coating covers all surfaces, including hole walls and edges, creating a smoother, more durable surface.

Nylophobic two-layer system. The same full nylon coverage and rounded edges, with a highly hydrophobic, low-adhesion, non-stick surface on top. Water and liquids bead up and roll off instead of sitting on the part.

What the system delivers

  • Highly hydrophobic: water and liquids bead and release easily
  • Ultra-low surface friction: helps prevent sticking, buildup, and product loss
  • Durable nylon foundation: thick coating protects the metal and softens sharp edges
  • Built for perforated metal: 100% coverage, including hole walls and edges, for smoother flow and easier release
  • Chemical and corrosion resistant: helps extend service life in tough environments

Is Nylophobic right for your part?

Nylophobic is built for perforated metal components where both surface performance and edge protection are critical. If your screens, trays, or guards are catching product, holding moisture, or corroding at the holes, send us the substrate, the perforation size, and the environment the part lives in. We will tell you whether Nylophobic is the right fit and what the finished dimensions will look like.

Jim Stuelke is CEO of Extreme Coating Solutions in Kansas City, an applicator of functional coatings since 1959.

info@extremecoatingsolutions.com  •  816.381.9901  •  www.extremecoatingsolutions.com
Most chemical- and corrosion-resistant coatings fail the same way. Water sits, then evaporates, but the Salts stay. The coating film is still on the part, but the electrolyte is now living on top of it.

Hydrophobicity is how you interrupt that sequence.

How Hydrophobic Coatings Change the Way Corrosion Starts

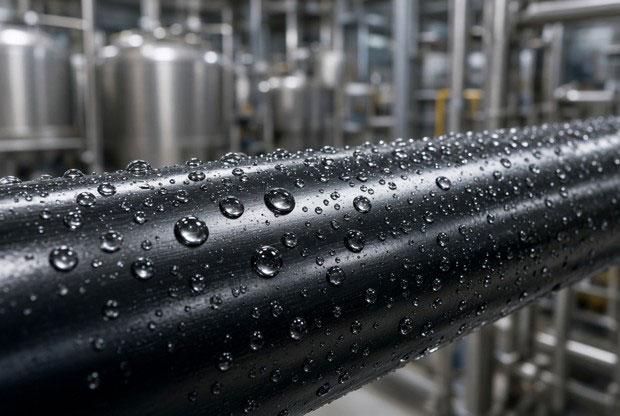
If water cannot wet the surface, it cannot easily feed the corrosion cell.

The coating is not the whole story

At Extreme Coating Solutions, we apply functional coatings. That means the film has a job: release, barrier, heat management, chemical resistance—or some combination.

A good barrier chemistry still needs help if process water, wash chemicals, or coastal salt can dwell on the surface. That is why we often put a hydrophobic topcoat over an already-capable system. The base coat handles adhesion and chemistry. The hydrophobic layer cuts wet time and keeps contaminants from hanging on.

Four things hydrophobicity actually does

  • Breaks the water film. No continuous electrolyte, fewer electrochemical cells on steel, aluminum, and brass.
  • Reduces deposit dwell. Salts, splash chemicals, and process residue have less time to sit and concentrate.
  • Self-cleans under flow. Droplets roll and take dirt with them. Less wash frequency. Fewer defects under trapped soil.
  • Tightens the barrier. Highly crosslinked siloxane and silazane networks resist water and ion permeation. Thickness still matters. Hydrophobicity makes that thickness work harder.

It is not a substitute for the rest of the system

Contact angle does not fix poor adhesion. It does not forgive the wrong resin in strong acid. It does not replace film build.

Before we add a hydrophobic layer, we still ask:

  • What is the substrate?
  • Splash, vapor, or immersion—and at what temperature?
  • Which chemicals, at what concentration and pH?
  • Does the part flex, abrade, or thermally cycle?
  • Is PFAS-free, food-contact, or a specific VOC limit required?

Then we validate. Salt fog or CASS. Chemical spot or immersion. Adhesion. Abrasion. Flexibility. A single coupon test is not a specification.

In coatings, a coupon is a small, flat sample panel (often a few inches square) made from the same substrate as the real part, such as steel, aluminum, or brass. The panel is prepped and coated exactly the way the production part would be, then put through a test in place of the actual part.

Where plants actually use this

Chemical processing. Acid and brine films on piping, flanges, and tank exteriors. Hydrophobic topcoats keep splash from sitting at welds and fasteners.

Food processing. Washdown chemicals and product residue on frames, hoppers, and rollers. Low-energy films shed water and soil—when the chemistry matches the contact class.

Tooling and rollers. Mold water jackets pit from chlorides and MIC. Tool faces pick up flash. One hydrophobic system can cut both corrosion and buildup.

Marine and coastal. Salt aerosol never dries. Reducing chloride dwell extends the time between wash-and-touch-up cycles.

Fleet and polished aluminum. Road salt and high-pH washes stain and pit wheels, tankers, and trailers. A clear hydrophobic film protects reflectivity without a heavy pigmented coat.

Cooling water and wastewater. Biofilm plus chlorides is a corrosion accelerator. Hydrophobic walls are harder for microbes and deposits to colonize.

Oil, gas, and energy. Produced-water splash and coastal skids. Under-deposit corrosion is where coatings usually fail first.

Aerospace and composite tools. Moisture in cooling passages and on mold faces drives pitting and vacuum leaks. Thin hydrophobic sealers protect the metal and keep release surfaces cleaner.

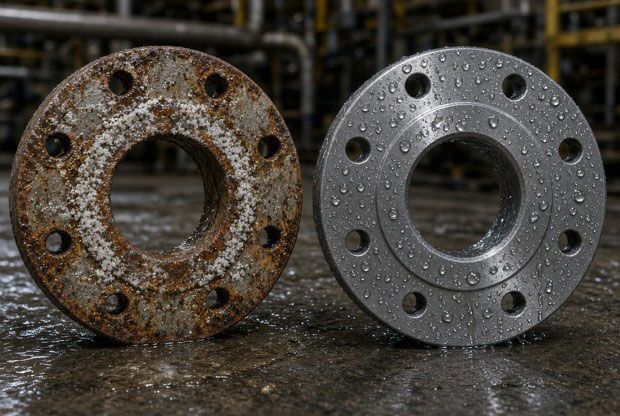
Same environment. Different surface energy.

How Hydrophobic Coatings Change the Way Corrosion Starts

The question we ask customers

We don’t ask, “Is the coating hydrophobic?”

We ask this: “Does hydrophobicity, on this chemistry, on this part, cut wet time and permeation enough to move the failure date?”

That is a measured answer. We run the tests in-house so we are not guessing from a data sheet.

If a part is staining, pitting, or picking up residue between wash cycles, send the substrate, the chemical list, and the temperature. We will tell you whether a hydrophobic upgrade is worth the film build—or whether adhesion and barrier chemistry need to be fixed first.

Jim Stuelke is CEO of Extreme Coating Solutions in Kansas City, an applicator of functional coatings since 1959.

info@extremecoatingsolutions.com  •  816.381.9901  •  www.extremecoatingsolutions.com
ECS’s Testing Capabilities Provides Peace of Mind for its CustomerExtreme Coating Solutions (ECS) operates multiple salt fog chambers to perform accelerated corrosion testing in accordance with ASTM B117. First published in 1939, ASTM B117 remains one of the most widely recognized and trusted corrosion test standards in use today.

For high‑performance organic and polymer coating systems, however, traditional salt fog testing can be time‑prohibitive. Validating premium systems often requires 1,000–4,000 hours of continuous exposure—equivalent to 41–170 days. In a market where product launches and design decisions move quickly, waiting several months for test results is often not realistic.

The Challenge: Fast Answers Without Compromising Confidence

A recent project illustrates this challenge. Our client was developing a coating system consisting of:

  • A clear powder coat applied over polished aluminum
  • A silane‑family clear coating as the final topcoat

Their original powder/silane system had already demonstrated excellent performance: more than 3,400 hours in ASTM B117 salt fog with acceptable results. The client now wanted to switch to a different powder coating chemistry but needed to understand:

  • Would the new powder chemistry maintain the same level of corrosion resistance?
  • Could they make this decision on a much shorter timetable than another 3,400+ hour test?

They needed reliable data long before a full 142‑day salt fog exposure could be completed.

Considering an Alternative: CASS Testing

To address the schedule constraint, ECS proposed incorporating a CASS (Copper‑Accelerated Acetic Acid Salt Spray) test following ASTM B368 as an additional tool.

For aluminum substrates, CASS testing is significantly more aggressive than standard salt fog. As a result, it can generate comparable failure modes much faster. As a rule of thumb, CASS can be up to eight times faster than ASTM B117 salt fog on aluminum—compressing what would be 142 days of exposure into roughly 18 days.

An uncoated aluminum panel placed in our CASS chamber for just under 48 hours showed extensive corrosion, clearly demonstrating the severity and efficiency of the test.

ECS’s Testing Capabilities Provides Peace of Mind for its Customer ECS’s Testing Capabilities Provides Peace of Mind for its Customer

However, there is an important limitation:

  • ASTM B117 and ASTM B368 are not interchangeable.
  • The “8× faster on aluminum” relationship is only a rough guideline and is not sufficient by itself to justify a major material or process decision.

To be responsible, any use of CASS as a time‑saving tool must be backed by data that correlates CASS performance with traditional salt fog results for the **specific** coating systems under consideration.

Building a Data‑Driven Test Matrix

To mitigate risk and provide a defensible basis for the client’s decision, ECS designed a targeted testing matrix.

1. Coating Variants Tested

We prepared panels using the existing silane‑based topcoat over:

  • The original powder coating chemistry (baseline, previously qualified at 3,400+ hours in B117)
  • The new powder chemistry, in two versions:
    • With an adhesion promoter
    • Without an adhesion promoter

2. Adhesion & Interface Modeling

Before testing, our team developed computer simulation models to predict how the silane‑based clear coat would interact with the new powder chemistry. The modeling indicated that:

  • The new powder system would likely require an adhesion promoter to achieve robust inter‑coat bonding.
  • Without an adhesion promoter, the interface could become a weak link under corrosive conditions.

These insights informed the test matrix and allowed us to focus on the most critical variables.

3. Parallel Testing: CASS and Salt Fog

We then ran two identical sets of panels:

  • One set in our CASS chamber (ASTM B368) for rapid, accelerated comparison.
  • A second set in our salt fog chamber (ASTM B117) as a longer‑term validation and correlation tool.

The objective was not to replace salt fog testing with CASS, but to establish whether CASS results for this specific system could be relied upon to make an earlier, informed decision—then confirm that decision as the longer B117 test progressed.

Outcome: A Confident Path Forward

In a twist typical of real‑world projects, the client’s product launch was ultimately delayed long enough to nearly coincide with completion of the extended ASTM B117 test.

By that time:

  • The CASS and salt fog results were in strong agreement.
  • Both test methods confirmed that the new powder chemistry, when used with the adhesion promoter, delivered performance comparable to the original, previously qualified system.
  • Panels using the new powder without the adhesion promoter did not perform to the same standard, validating the importance of the promoter identified by our modeling work.

Armed with correlated data from both CASS and salt fog testing—and a clear understanding of the role of the adhesion promoter—our client was able to confidently move forward with the new powder coating chemistry while maintaining the corrosion performance their customers expected.

ECS: Integrated Testing, Analysis, and Development Support

Extreme Coating Solutions maintains a broad range of analytical and testing capabilities to support:

  • Quality assurance and validation
  • New coating product development
  • Failure analysis and troubleshooting
  • R&D and process optimization

Our lab equipment and services include, but are not limited to:

  • Thermo Fisher iS10 FTIR spectrometers
  • Corrosion testing (ASTM B117, ASTM B368, and others)
  • Adhesion, hardness, and chemical resistance testing
  • Custom test matrix design and data interpretation

If you’re evaluating new coating chemistries or need to compress development timelines without sacrificing confidence, ECS can help design a test strategy that balances speed, cost, and risk.

For more information, contact:

Jim Stuelke, CEO
Phone: 816‑381‑9901
Email: info@ecs-ww.com

CHROMASLICK™ OUTPERFORMS VARIOUS PTFE-BASED COATINGS IN SIDE-BY-SIDE CHEMICAL CORROSION TESTINGBy Jim Stuelke, CEO of Extreme Coating Solutions

CHROMASLICK™ is ECS’s product offering for projects requiring non-stick/high-release, excellent chemical and environmental corrosion-resistance, excellent UV-resistance, and… can be offered in pretty much any color needed.

In this case, CHROMASLICK™  was applied to the client’s operating component and tested against various PTFE-based coatings, all of which ended up falling short of the results shown by our CHROMASLICK™ product.

What is CHROMASLICK™

CHROMASLICK™ is a 2-coat system utilizing one of the polysiloxane pigmented base coating products from suppliers like PPG, Sherwin Williams and others. These coatings by themselves are outstanding product technologies, possessing some of the following properties:

Abrasion resistance (ASTM D4060, 1 kg load/1000 cycles, CS-17 wheel): ~53 mg weight loss reported for PSX 700.

Adhesion (ASTM D4541): ~2700 psi on steel (≈18.6 MPa) quoted for PSX 700.

Elongation (ASTM D522): ~14 %.

Weathering/Corrosion: Example: Salt spray (ASTM B117) 5500 h with no face corrosion/blistering reported in one data sheet. Humidity (ASTM D2247) also 5500 h with similar result.

Excellent UV-resistance for gloss and color retention

CHROMASLICK™ OUTPERFORMS VARIOUS PTFE-BASED COATINGS IN SIDE-BY-SIDE CHEMICAL CORROSION TESTING CHROMASLICK™ OUTPERFORMS VARIOUS PTFE-BASED COATINGS IN SIDE-BY-SIDE CHEMICAL CORROSION TESTING

How do we improve and add to these performance properties?

By top coating it with patented hybrid polysilazane-polysiloxazane clear coatings provided by Dyna-Tek, LLC. using their SlickShield™ PLUS product combined with our proprietary pretreatment process.

SlickShield™ PLUS adds several very important performance properties to the polysiloxane base coat:

  1. Significant increase in PERMEATION resistance.
  2. Adds excellent hydrophobic properties.
  3. SlickShield™ PLUS itself has outstanding corrosion resistance that further compliments the polysiloxane base coat.
  4. Excellent inter-coat adhesion via a covalent bond, which significantly enhances the combined properties of both coatings.

Anyone who knows the polysiloxane coating chemistries well, knows that they inherently have a “low surface energy”, which can sometimes lead to inter-coat adhesion with other, dissimilar coating chemistries.

Our proprietary processes not only overcome any possibility for inter-coat adhesion issues but results in a “covalent bond” between the two.

For more information, email us at sales@ecs-ww.com or call us at 816.381.9900.

ChromaSlick™Armed with the confidence of a successful 10-year, proven track-record of usage in various industries to control adhesive build-up, Extreme Coating Solutions (ECS) is now expanding its ChromaSlick™ coatings offerings into new markets.

ChromaSlick has excellent corrosion-resistance exhibiting over 5,000 hours of Salt Spray (ASTM B1117) testing with no visible corrosion or blistering. ChromaSlick’s combination of Easy Clean/non-stick and corrosion resistant properties makes it well suited for uses on components found in areas such as:

  • Industrial plants – Ink trays, rollers, any surfaces where an easy clean surface can minimize down-time.
  • Transportation sectors – components like grills, bumpers, and ancillary items found on buses, trucks and rail products.
  • Marine – components that not only see marine corrosion but also abrasive use.
  • Indoor aquatic centers and sports stadiums
  • Any products subjected to the corrosive environments found near coastal developments
  • Offshore oil, LNG platforms, FPSO’s and exterior of tankage

Product information

ChromaSlick is a multi-coat organosilicon hybrid system that exhibits excellent non-stick properties, robust chemical resistance and very good UV-resistance for color and gloss retention.

Performance properties include:

  • Continuous operating temperature resistance is 250 – 275℉.
  • Graffiti resistant.
  • Good abrasion-resistance.
  • Coefficient of friction of .02-.03

NOTE: ChromaSlick is currently not approved for food-contact surfaces.

For more information about ChromaSlick™ or email us at sales@ecs-ww.com, or feel free to call us at 816.381.9900.

What is PFOA and why has it become a 4-letter word?

What has long been viewed as an irreplaceable solution in the coatings industry, “PFAS” has become a “4-letter word”

Even if you’ve never heard of the chemical “PFAS”, your world is currently being affected by it. PFAS (per- and polyfluoroalkyl substances), also frequently called “forever chemicals”, is a man-made chemical characterized by its strong carbon-fluorine molecular bond, which is one of the strongest molecular bonds in all of chemistry.

This strong molecular bond is significant to PFAS’s almost unrivaled chemical resistance to a broad range of acids, solvents and other chemicals that degrade not only other coatings, but also metals and materials. Ironically, the strengths of PFAS in coatings are how it comes to be known as a “forever chemical”.

While the PFAS in/on common products stands up to environmental degradation longer than most, their degradation is slow and continuous. This leads to their accumulation in soil, water, and living organisms. PFAS exposure has been linked to adverse health effects, including cancer, hormonal disruption, immune system suppression, and developmental issues in children.

PFAS Alternatives

Some of our customers have already asked us to guide them on converting their coating specifications to PFAS-Free alternatives. In each case, we have found them at minimum, new coatings that are equivalent to their PFAS-based predecessors, and in several cases the new coating solutions have benefits they didn’t have before.

We will be publishing case studies about these success stories soon. However, feel free to reach out to us if you would like to explore PFAS-free options as well!

We can be reached at info@extremecoatingsolutions.com or call us at 916.381.9901. You can also find us online at www.extremecoatingsolutions.com

One Million DollarsThe following is a list of important questions related to your current investment in molds and tooling:
  • How much are you spending on molds/tooling each year?
  • Are they lasting for as many production cycles as they were engineered for?
  • Does your company measure the number of production cycles your molds produce versus the projected number of cycles the tooling manufacturer made when you were evaluating the payback analysis?
  • What is the true cost per production/part cycle versus the real “life cycle” of the tooling?
  • How can we save you $1 million dollars in a year?

Companies that manufacture molded products that include “sticky” ingredients such as candy (basically any product with sugar), adhesive-backed printed labels, or the latest generations of high-performance aerospace composite resins (like those used to mold the fuselage spars and components for the Boeing 787…) ALL of these processes inevitably lead to sticky production issues, quality control problems, and lost profits when production is halted due to molds sticking to the molded parts as the original mold release/non-stick coatings wears off.

The tooling manufacturer isn’t necessarily at fault if the manufacturer doesn’t properly maintain the non-stick coating on the tooling. After all, metal is stronger than any non-stick coating… so, when the coating wears off, wear and tear accelerates.

Improving the Efficiency of Tooling

ECS works with a broad range of clients who recognize the value of keeping their tooling working efficiently by having their molds recoated with non-stick coatings ranging from PTFE-based fluoropolymers to Sol-Gel technologies. Some of these clients cycle their tools out frequently, sometimes several times a month to be recoated. The problem this can create however, is when the worn coating is blasted off to prep for a new application, the blasting process is slowly eroding the metal below it also.

Over time, the erosion is enough to render the tooling dimensionally obsolete and the tooling scrapped. To overcome this, we utilize walnut blast media to remove the original coating instead of blast media. Because the walnut media is harder than the coating, but softer than the metal, there is no erosion.

While we charge slightly more for this process, the tooling’s operational life is extended significantly. In a recent case study, whereas our client had been replacing the tooling each year, they have extended it to two years… and counting. We saved them the equivalent of $1 million because they don’t have to buy replacement molds as often.

How much money can we save your company? Let’s talk.


With all the challenges (everyone) is facing in this world, it’s important to make space for our teams to spend time together and blow off some steam. To talk about something besides work. It’s in these moments that deeper bonds are built and strengthened.

For this event, I turned to Jason Terry, the founder and owner of Blue Gurus, our social media advisor, trusted friend, and Bourbon Connoisseur. Jason volunteered to come by our place and conduct a Bourbon Tasting.

“I’ve been working with Jim and the ECS team for many years. Over the past couple of years, Bourbon has become a passionate hobby for me and I love sharing the experience with others.

I decided to bring an interesting selection of bottles. Some lower proof, some higher. Some easy to get at the local liquor store, some not so much. In the end, everyone had a couple of favorites and not everyone agreed on what was best. And that’s one of the best things about Bourbon. Every person will have their own preferences, and some of the fun is comparing notes as you try different bottles.”
Jason Terry, Blue Gurus

Coatings, Cocktails and Cigars

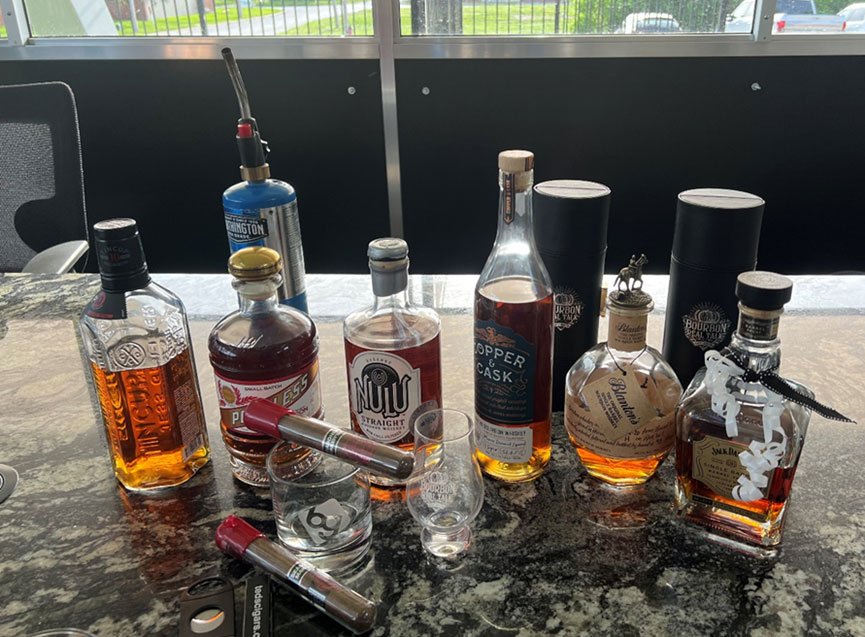
As you can see, Jason brought a great selection of Bourbons to compare and pick our personal favorites.
From Left to Right: Tin Cup 10 Year Whiskey, Peerless Single Barrel, Nulu Straight Single Barrel, Copper & Cask Missie’s Store Pick, Blanton’s 10 Year Single Barrel, Jack Daniel’s Single Barrel

We also rounded out the tasting with some bourbon-infused cigars. Why the propane torch you ask? Well, none of us had a lighter and the matches we had were old, so we had to improvise.

Our next group gathering idea?

We are taking everyone to the shooting range at Frontier Justice so everyone can receive safety training on how to handle different types of pistols, and of course, blast some targets. There won’t be any Bourbon at this event…

As we come up on Memorial Day weekend, we hope all of you are finding time to not only smile, laugh, but also take the time to reflect and appreciate the sacrifices of all members of the U.S. military who died while serving and protecting the privileges we have as Americans. God Bless.

– The Extreme Coating Solutions Team

FDA LogoWhat does it mean to be Food-Grade?
Food grade means that the material is either it is okay to come into direct contact with food products or the substance is safe for human consumption.

What does Food Safe mean?
Food safe means that a Food-Grade material is also suitable for its intended use and will not create a food-safety hazard.

What are Food Contact Surfaces?
A food contact surface is any surface that may come into direct contact with food. Food contact surfaces are made of food-safe materials designed to withstand the environment where they will be used. This includes exposure to cleaning compounds, sanitizing agents and cleaning procedures.

What does GRAS stand for?
GRAS is a substance that is Generally Recognized as Safe. These are materials that can be safely used for articles and surfaces that come into direct contact with food under normal, Good Manufacturing Processes (GMP).


How do I know which type of standards my product needs?

One place to start when figuring out if you need a coating that is GRAS, Food-Grade, or Food-Safe coating for your product is to know which type of contact your product makes with the food you’re working with or around. When dealing with the world of food, the regulations can get specific as a safety precaution against potentially consuming something that may cause someone to get sick.

This is partly why there are Three Types of Food Contact.

Direct Contact substances are those that directly touch, or contact, food. This may lead to the creation of direct or indirect food additives.

Indirect contact Substances might come in contact with food, such as on the outside of food packaging; such as a sealed packaging or a carton.

Incidental contact substances are those that rarely contact food and the contact is not purposeful or continuous. For example, food that contacts an extraneous part of a food processing machine where contact is not expected is considered incidental.

If your product falls in the Direct Contact description you may have noticed that your product may or may not be considered a potential food “additive”. What do you mean I could be creating a food additive?

Thankfully there are only two types of food additives recognized by the FDA.

Generally, they define an additive as: “any substance the intended use of which results or may reasonably be expected to result, directly or indirectly, in its becoming a component of, or otherwise affecting the characteristic of any food including any substance intended for use in… packing…or holding food…”

This just means that whether or not you mean to, your product or coating might get added to the food you are helping to produce or manufacture. The USDA and FDA make this part easy as they both manage different aspects of potential food-related contact. Think of them as two separate sides of the same coin.

  • The most common type of FDA-approved coatings are intended to come into direct or indirect contact with food substances.
  • USDA approved coatings will typically be wall and floor coatings. The latter type—especially floor coatings—is specifically formulated to handle the extreme cleaning conditions that are usually present in a food and beverage facility.

When it comes to direct contact with food or working in and around a food production facility a little bit of knowledge about your coating needs goes a long way. Whether your product requires a Food-Grade, Food-Safe, or even Generally Recognized as safe we’ve got you, and your product, covered.

Angela ConrowBy Angela Conrow, Controller at Extreme Coating Solutions
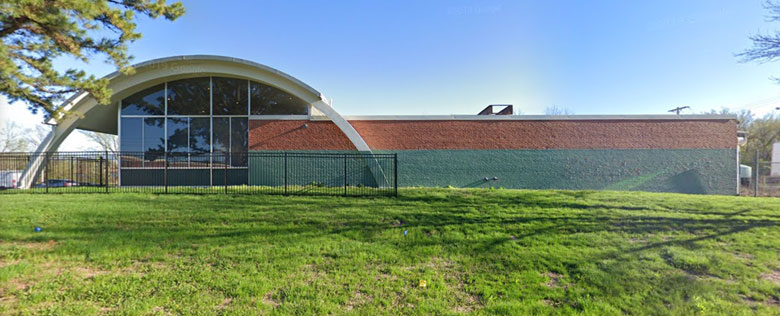
Since moving Extreme Coating Solutions into its current location in 2017, we have continued to make improvements to the building. Things like replacing the roof, new HVAC units, windows, as well as leasehold improvements for projects like our new coatings manufacturing capabilities which is part of a collaboration with another company; Dyna-Tek.

Our “Googie” Karma

Built in 1959, our building’s unique architectural style stands out among the other more conventional manufacturing buildings in our area. While struggling to describe our facility recently, I mentioned to our team that our building’s architecture was “reminiscent of the Googie Modern Architecture style from the mid-nineteenth century”.

What? Googie?!

My team decided to look that one up. Sure enough Google reported, “Googie architecture was considered futuristic architecture and was influence by the car culture, jets, the Space Age and the Atomic Age.” I not only gave a really good trivia question for future reference, but we all think it’s cool karma that in our 1959 Googie, jet-influenced architecture, we’re manufacturing coatings for the aerospace industry today!

Extreme Coating Solutions - Googie Architecture
Facility Upgrades

In a long-overdue move, we recently upgraded the facility security systems and added new receiving lobbies for both the office and shipping entrances. To guide us on this, we called on Kenton Brothers Systems for Security to recommend and install new exterior and interior access controls, video surveillance and a commercial grade intercom system. Kenton Brothers came through with flying colors and we have been very pleased with the results.

One area of improvement that has been really appreciated has been the video-intercom system.

In the past, incoming truck drivers had to go up to our exterior dock door, ring our buzzer and then wait for us to come and open the door. This wasn’t a good scenario, particularly when it was raining, snowing or just plain hot. With the new security measures, drivers come into the new shipping and receiving room and go to the AXIS video intercom which is tied to our IT/phones and enables someone from our office staff to greet and take care of them.

ECS Building Signage ECS Building Signage

Building Signage

We had never gotten around to adding building signage since moving into our current building back in 2017. Our CEO, Jim Stuelke, would jokingly say we didn’t need it… “just tell visitors to look for our building’s white arches… Just like “McDonalds” only white. You can’t miss us!”

I recently had my 1-year anniversary with ECS and moved ahead with adding building addresses… Next month we’ll be official when we put our name up on the side of the building after it gets a new coat of paint courtesy of our friends at Major Painting Co.

Unfortunately, the COVID impact hasn’t allowed us to have many visitors to share all of this with, but the ECS team has enjoyed the updates. As far as company culture, we’re always looking to improve. And we feel our facility should reflect that as well!